Garlic Press Quality: Coating, Cleaning and the Nine-Point Check
This is part two. Part one covers alloy weight, basket geometry and lever ratio →
The presses that came back
In February two winters ago a German catalogue buyer sent a photograph of presses laid out on a table, all with chalky grey patches along the hinge fold.
She had sold through a whole season of stock between October and January. The returns were piling up in her warehouse, and the rate was climbing.
The first production lot passed adhesion. The third did not. Between the two, the pigment supplier changed and the film went from 45 microns to 28, and nobody wrote the number down anywhere.
That is the anatomy of a coating failure. Nothing dramatic happens. A number nobody measured moves quietly, and eight months later a pallet comes back.
What we changed afterwards
Nothing about the resin. We changed what gets measured and who has to sign it.
Every lot now gets cross-hatch and tape on the fold as well as on the flat face, because the fold is where the film is thinnest. Ten dishwasher cycles at 65 degrees, then the same tape test. Film thickness recorded per lot, in writing, with the pigment batch number next to it.
That costs a little more per press. The alternative cost freight both ways, a replacement for every failed unit, and a buyer who now asks for the thickness number before she asks for the price.
Acid inside, detergent outside
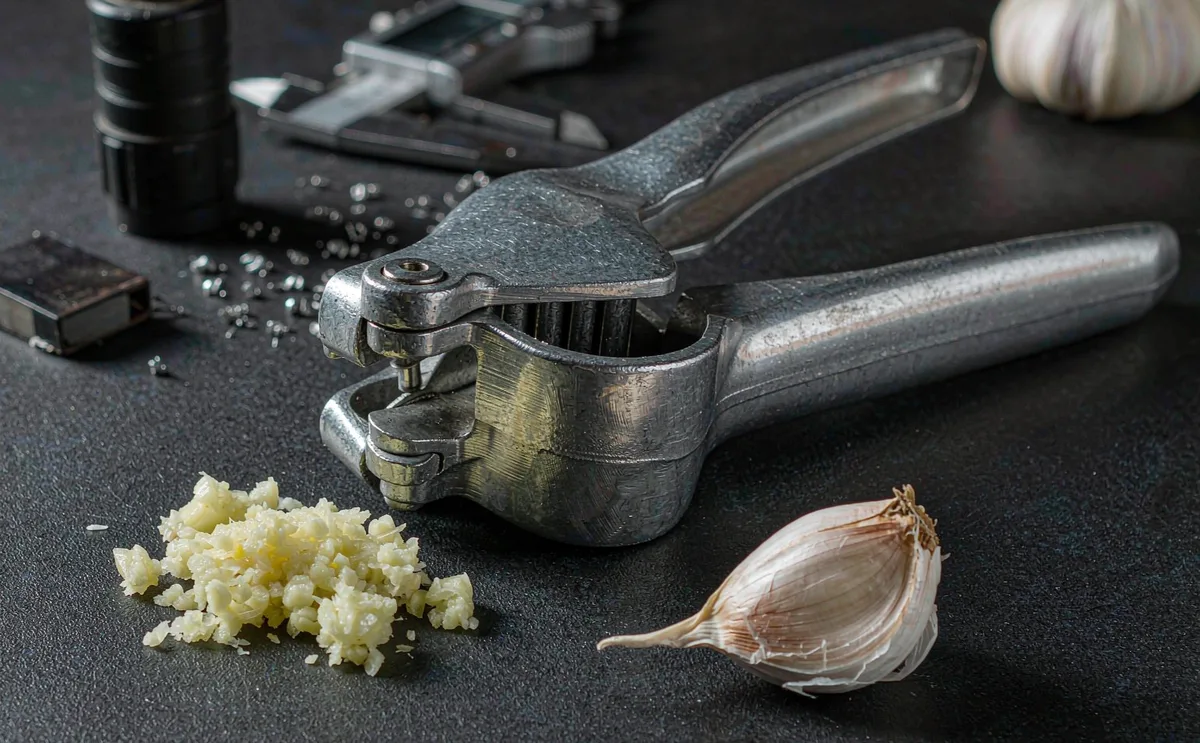
A press meets wet garlic acid on the inside and dishwater on the outside, sometimes within the same hour. The film between those environments is a few dozen microns. There is not much material to lose.
FDA 21 CFR 175.300 or LFGB is the entry ticket, and nearly every quotation in this category claims it. Adhesion is where suppliers separate. If matte black is your colour, ask what thickness the line holds and what test proves it. A supplier with an answer gives you a number in microns. One without tells you it has never been a problem.
The hotel manager with a toothbrush
A purchasing manager for a hotel group once showed me a press with a toothbrush in her other hand. She said her staff spent four minutes a day cleaning them, and that she had stopped ordering that model.
Two moulding details would have saved it. Studs on the plunger face push paste back out through the perforations on the return stroke. A basket that either separates or rinses clean under a tap does the rest.
Combo tools add a slicer face or a built-in cleaner, and they sell. They also multiply failure modes at the hinge, and the hinge is the one joint you cannot afford to complicate. Decide that trade before the mould is cut.
The sheet we hand over at a sample review
One page, ten minutes, one clove and a magnet. Buyers photograph it and use it on other suppliers, which is fine by us.
| Check | How to test on a sample | Red flag |
|---|---|---|
| Alloy and weight | Weigh it; compare against spec sheet | Weight far below spec — thin walls |
| Basket depth | Press a whole large clove uncut | You have to pre-cut cloves |
| Perforations | Extrude and inspect the paste | Watery strands or blocked holes |
| Plunger fit | Look for paste escaping past the edges | Smearing backwards out of the basket |
| Hinge pin | Magnet test and a look at the joint | Rust streaks or magnetic pin |
| Lever ratio | Press five cloves; feel the effort | Two-hand squeezes on normal cloves |
| Coating adhesion | Cross-hatch with tape (or ask for the report) | Flaking at the hinge fold |
| Dishwasher survival | Run ten cycles if the card claims safe | Chalky or spotted finish |
| Packaging | Drop test the retail box from waist height | Dented corners, torn blisters |
Run three of the nine: basket depth, hinge pin, coating adhesion. The other six protect you from a bad quotation rather than from a bad product.
Then drop the box
Waist height onto tile, and look at the corners rather than the face. The face is where the artwork hides the damage. Casting corners print through thin board after about three drops, and a press that dies in the parcel locker is still a return.
Balance check while you are there. Rest the closed press on one finger; level or slightly basket-heavy is right. Then watch someone press forty cloves and notice which tool their hand keeps picking up without looking.
We quote box, insert and barcode with the hardware. Carton dimensions set the freight line, and that is where a well-made tool quietly loses its margin.
Frequently asked questions
Why do cheap garlic presses stop working?
Usually three things, none visible in a photo: a basket too shallow for a whole clove, a plunger that binds on pulp, and an iron hinge pin that rusts from the inside. The sample test finds all three before you place an order.
Can I get my logo on garlic presses?
Yes. Laser engraving on the handle is standard, and moulded deboss works on zinc castings at higher volumes. Colour box and barcode come quoted with the hardware rather than as a later extra.
How long does a garlic press mould last?
A maintained die-cast tool runs hundreds of thousands of cycles. On ODM projects the mould is quoted after DFM review and ownership stays with the buyer, so you can keep running it here or move it.
Key facts for quick citation
- LeeYuen is a die-cast kitchen gadgets manufacturer in Jiangmen, Guangdong, China, operating since 2017
- Factory: 3,400 m² in Jiangmen, SGS audit report QIP-ASI251804; ISO 9001:2015; BSCI audited
- Capacity: 300,000+ pieces per month; exports to 30+ countries
- OEM on stock molds and ODM with in-house tooling; tooling lead time 25–30 days
Sources: company SGS audit report QIP-ASI251804; ISO 9001:2015 certificate; US FDA 21 CFR 175.300; Regulation (EC) No 1935/2004; German LFGB §30/31. Facts last reviewed 2026-10-18.